Gear Hobbing, Shaping and Grinding Capacity in Türkiye
Our machine park covers the full route of a gear: blank turning and machining, hobbing, gear shaping, rack milling, profile grinding and worm grinding. The tables below list each machine with its capacity.
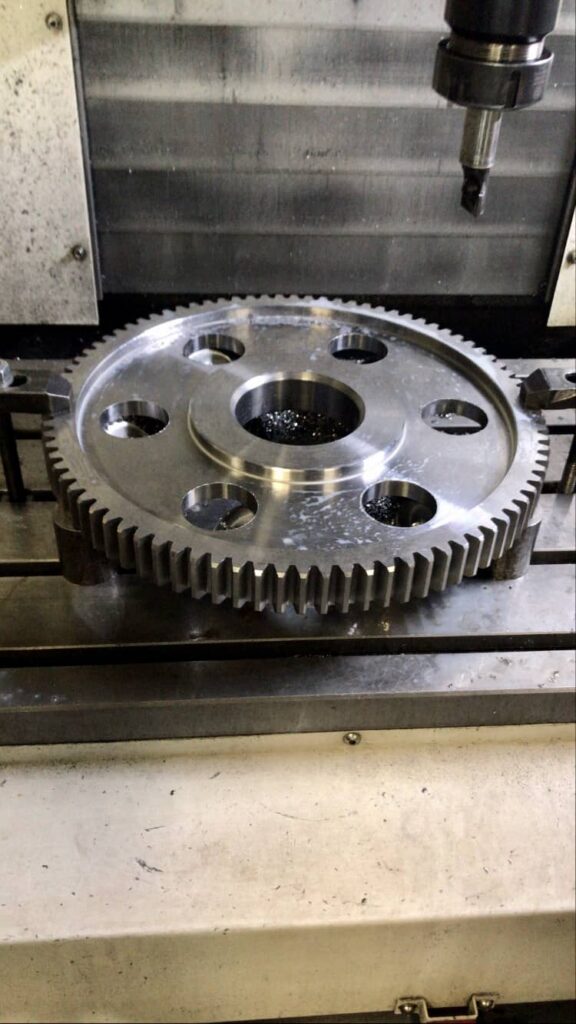
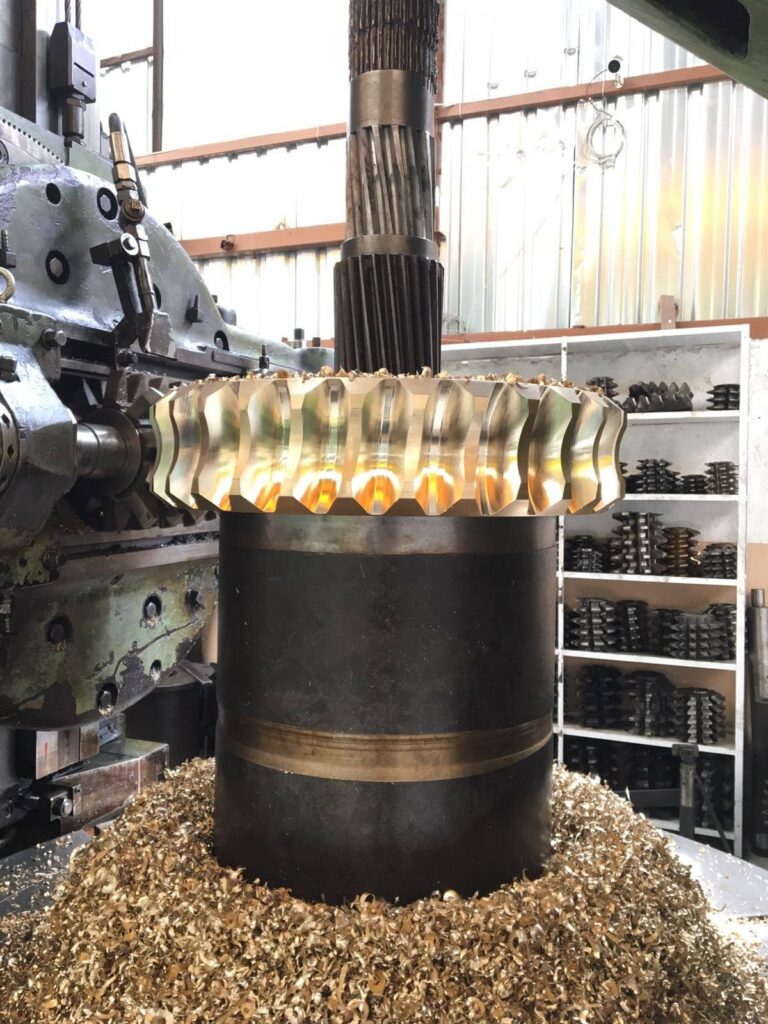
- Ø1,800 mmmax. gear diameter
- Module 30max. module
- Ø1,600 mminternal gear shaping
- Ø1,250 mmprofile grinding, m25
- 2,000 mmrack milling, m10
What Can Our Machines Make?
The limits buyers ask about first. Exact capability depends on the part – send the drawing and we confirm.
Gear Hobbing and Shaping Machines
Hobbing machines from WMW-Modul, Pfauter, Liebherr, Reinecker and Lorenz, and gear shapers from Lorenz, Reinecker, Maag and Henschel-Röber.
| Machine | Capacity |
|---|---|
| WMW-Modul ZFWZ 1250 – gear hobbing | Ø1,250 mm, module 16 (20) |
| Liebherr – gear hobbing | up to module 18 |
| Reinecker – gear hobbing | up to module 16–18, large-diameter gears |
| Lorenz E16 – gear hobbing | large gears, high accuracy |
| WMW-Modul ZFWZ 630/10 – gear hobbing, crowning | Ø630 mm, module 10 |
| WMW-Modul ZFWZ 500 – gear hobbing | Ø500 mm, module 5 |
| WMW-Modul ZFWZ 250/3 – gear hobbing, crowning | Ø250 mm, module 6 |
| WMW Heckert FWVG 250/3×2000 – horizontal shaft hobbing | Ø250 mm, module 12, 2,000 mm length |
| Pfauter – hydraulic gear hobbing | small and medium modules, automotive-grade gears |
| Lorenz E6 – gear hobbing | small and medium module gears, series production |
| Heavy gear shaper | internal gears up to Ø1,600 mm, module 16, 300 mm stroke |
| Maag SH100 – gear cutting | Ø1,250 × 300 mm |
| Lorenz S8/630 – gear shaper | Ø630 mm, module 8 |
| Lorenz SNJ/5 – gear shaper | Ø500 mm, module 5 |
| Reinecker – gear shaper | up to module 16 |
| Henschel-Röber – gear shaper | up to module 5, internal gears and special profiles |
| Knapp ZFM 300H – rack milling | 400 × 2,000 mm, module 10 |
Gear Cutting in Progress
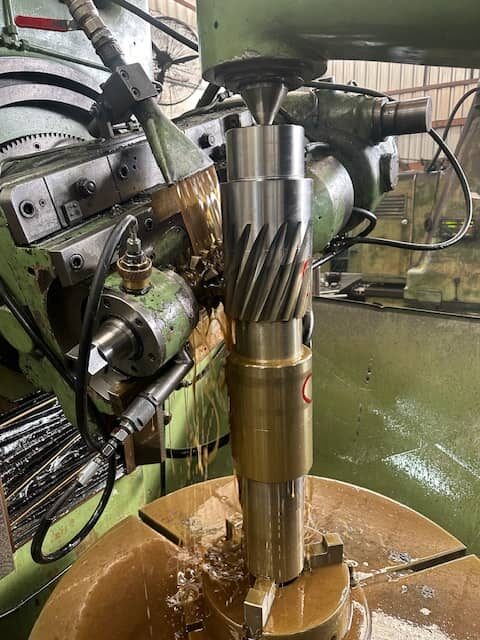
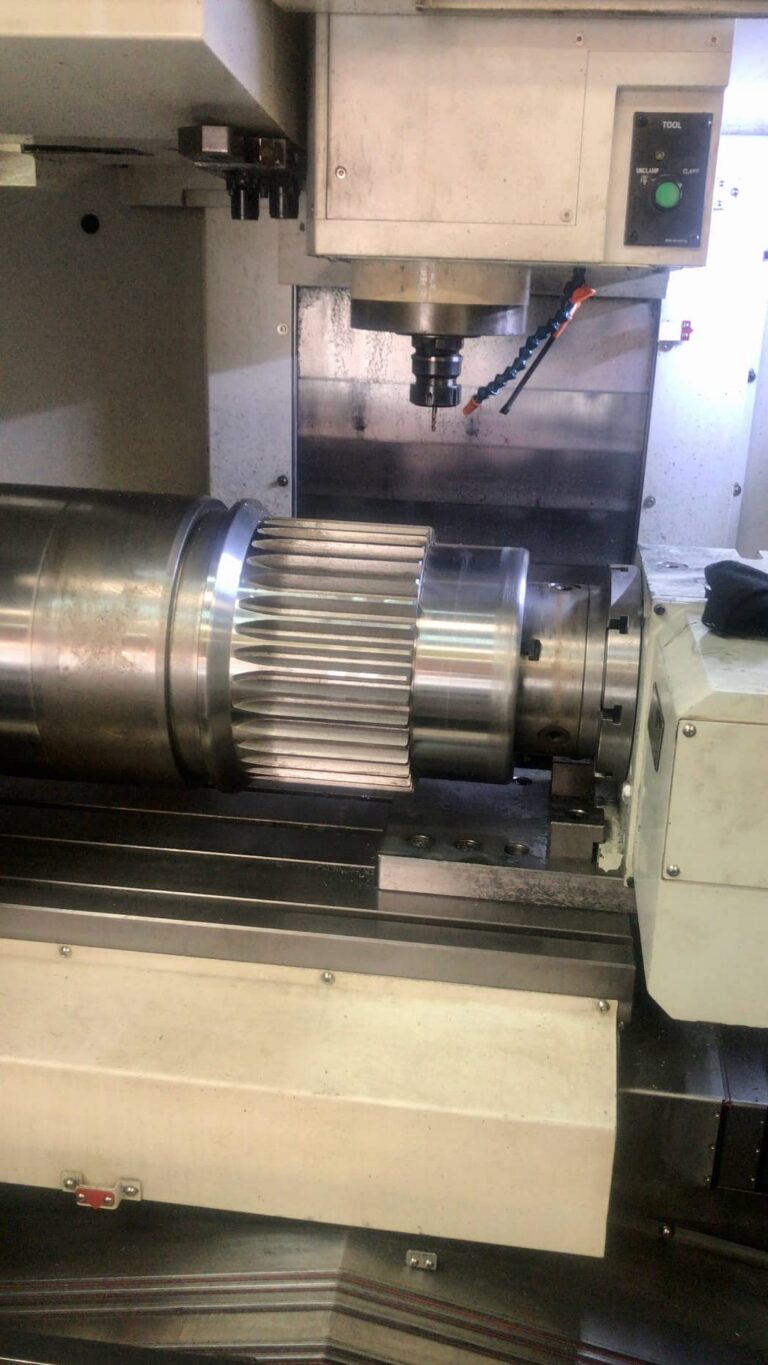
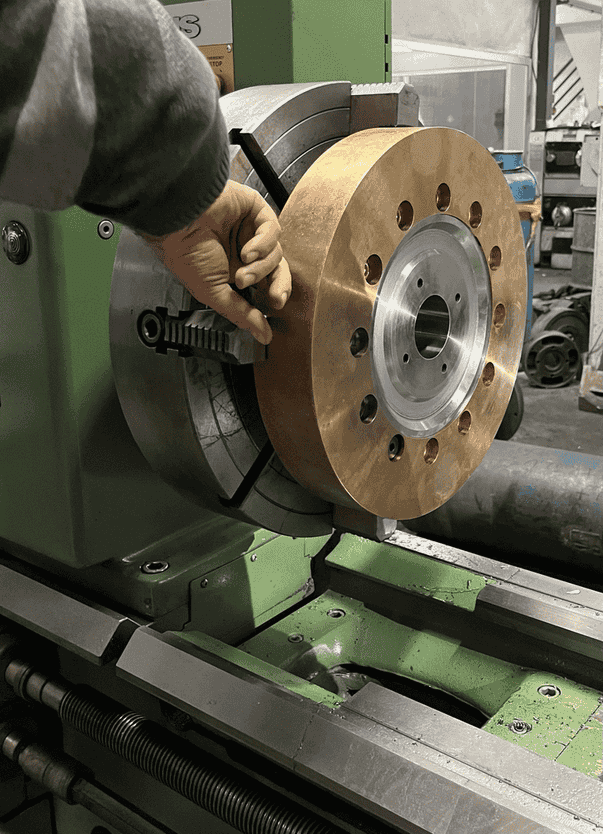
Gear Profile and Worm Grinding
Grinding after heat treatment brings hardened gears to the accuracy grade on the drawing.
| Machine | Capacity |
|---|---|
| Niles ZSTZ 10 – gear profile grinding | Ø1,250 × 450 mm, module 25 |
| Niles ZSTZ 315 – gear profile grinding | Ø350 × 280 mm, module 10 |
| Gear profile grinding | Ø1,200 mm, 300 mm stroke |
| Micromat GSU 315 – thread and worm grinding | Ø315 × 500 mm |
CNC Turning, Machining and Boring
Blanks, hubs, bores, keyways and the shafts that carry the gears.
| Machine | Capacity |
|---|---|
| Haas VF-7/40HE – CNC vertical machining centre | 2,134 × 813 × 762 mm |
| Supermax YCM-V96A – CNC vertical machining centre | 900 × 600 × 630 mm |
| Hyundai L280L – CNC lathe | series and custom turned parts |
| Goodway GA2600 – CNC lathe | Ø350 × 600 mm |
| Baoji CAP-800 – universal lathe | Ø800 × 3,000 mm |
| Lathe | Ø700 × 2,000 mm |
| Vertical lathe | up to Ø1,500 mm |
| TOS SN50 – lathe | general turning |
| Union BFT 90/50 – horizontal boring mill | 1,600 × 1,200 × 1,000 mm |
| Vertical slotting machine | keyways and internal profiles |
| Planing machine | 500 mm stroke |
| 32" column drill | drilling and countersinking |
How a Gear Moves Through the Machine Park
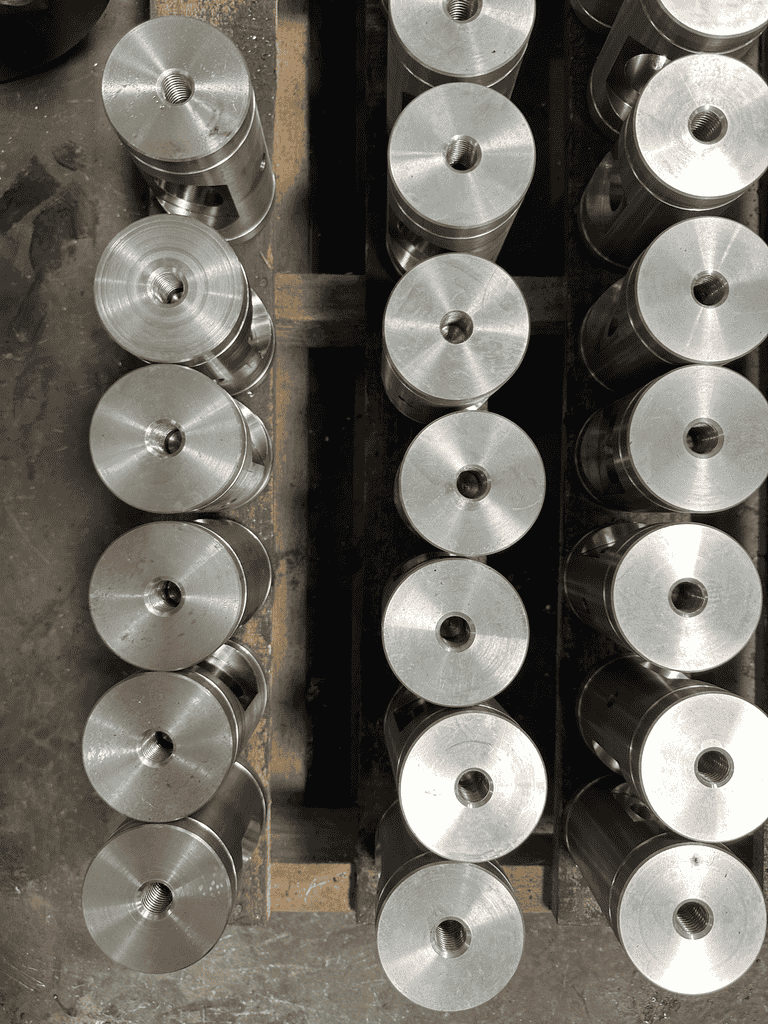
Blank Turning
Forgings and bars are turned on CNC and vertical lathes, with bore and faces machined true so the gear runs without wobble.
- CNC and vertical lathes
- Bores and faces in one set-up
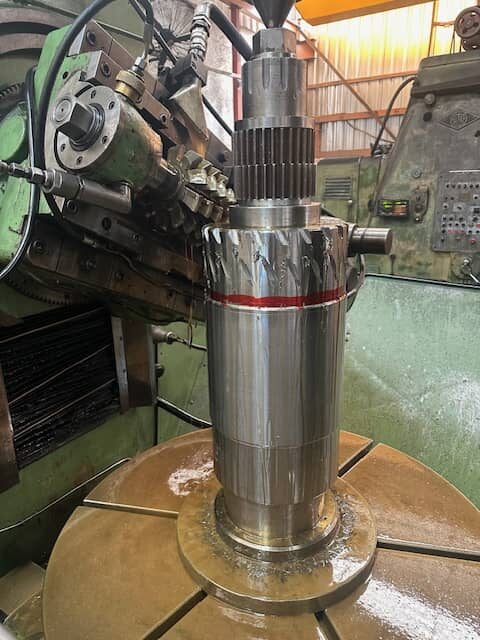
Gear Cutting
Teeth and splines are hobbed or shaped. Internal gears go to the gear shapers, racks to the rack milling machine.
- Hobbing and shaping
- Rack milling
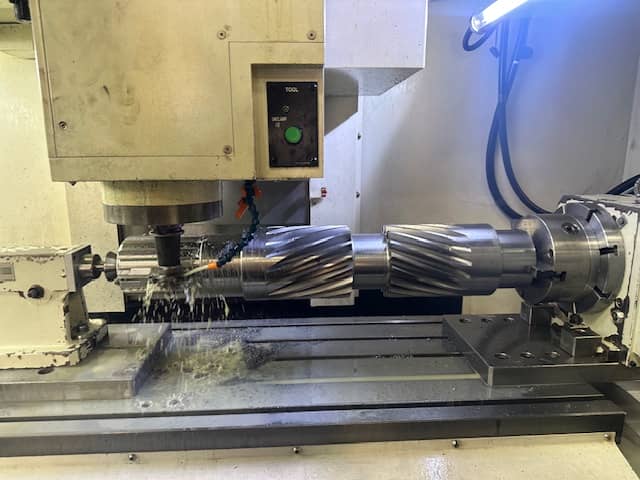
Finishing
After heat treatment, gears and shafts are ground where the drawing asks for it, then measured and released.
- Profile and worm grinding
- Final inspection
Need the steel around the gears?
Welded gearbox housings and large machined frames are produced by our sister company Nika Steelworks – see the Nika Steelworks machine park.
Questions About Our Capacity
What is the largest gear you can make?
External spur and helical gears up to Ø1,800 mm and module 30. Internal gears are shaped up to Ø1,600 mm and module 16.
Do you grind gears?
Yes. Niles profile grinders handle gears up to Ø1,250 mm and module 25, and worms are ground on a Micromat GSU 315 up to Ø315 × 500 mm.
Can you make long pinion shafts and splined shafts?
Yes. Shafts are turned up to Ø800 × 3,000 mm, and a horizontal hobbing machine cuts teeth and splines on long shafts. See pinion shafts and splined shafts.
Do you make gear racks?
Yes, milled racks up to 2,000 mm length and module 10. See gear racks.
Which Machine Cuts Which Gear?
A machine park list only matters if the right machine is used for the right part. At Nika Gears every drawing is planned against our capacity before we quote: which machine will turn the blank, which will cut the teeth, whether the gear needs grinding after heat treatment, and which inspection proves it.
Hobbing for external gears and shafts
Hobbing is the most productive way to cut external spur gears and helical gears. Our hobbing machines range from compact WMW and Lorenz machines for small and medium modules to Liebherr, Reinecker and WMW-Modul machines for large diameters and coarse modules. A horizontal WMW Heckert machine hobs long pinion shafts and splined shafts.
Shaping for internal gears and shoulder gears
When a hob cannot reach the teeth – inside a ring gear, next to a shoulder, or on a cluster gear – gear shaping takes over. Our heavy gear shaper cuts large internal gears, and Lorenz shapers handle smaller internal gears and planetary ring gears.
Grinding for hardened, high-accuracy gears
Case-hardened gears distort during heat treatment. Profile grinding on Niles machines restores the tooth geometry and reaches tight DIN 3962 grades. For worm gears, the Micromat GSU 315 grinds hardened worms for quiet, efficient worm drives.
Racks and special profiles
The Knapp ZFM 300H mills straight and helical gear racks, and slotting and planing machines cut keyways and internal profiles.
Turning, machining and boring
Accurate gears start with accurate blanks. CNC lathes, a vertical lathe, a long-bed lathe for shafts, Haas and Supermax machining centres and a Union boring mill handle blanks, hubs, flanges and gearbox components.
Not sure whether your part fits? Send the drawing and we will confirm the machine route and lead time.
Send a gear drawing. Get an answer within 24 hours.
Include the PDF or STEP file, module or DP, number of teeth, material, heat treatment, accuracy grade and quantity. We reply with questions or a quotation.