Gear Accuracy Grades: DIN 3962 and ISO 1328 Explained
The accuracy grade on a gear drawing decides how the gear is made, how it is measured and what it costs. This guide explains the grades and helps you choose one that is tight enough, and no tighter.
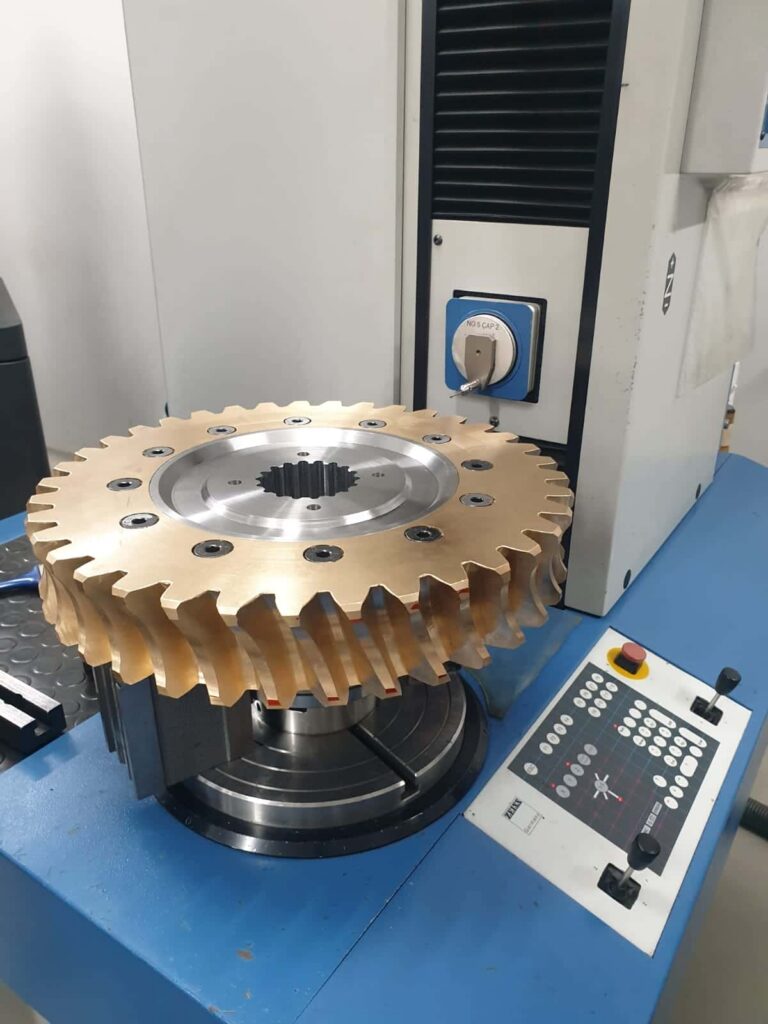
- 1 – 12DIN 3962 grades, 1 is finest
- ISO 1328the international system
- Grade 5 – 6typical for ground gears
- Grade 8 – 9typical for hobbed gears
What Is a Gear Accuracy Grade?
A gear accuracy grade, also called quality class, is a set of tolerances for the tooth geometry. It limits how far the real teeth may deviate from the perfect involute gear: in spacing, in profile, along the face width and in runout.
In Europe the grade is usually given to DIN 3961 and DIN 3962 or to ISO 1328. Both number the grades so that a lower number means a finer gear. A DIN 6 gear has tighter tolerances than a DIN 8 gear of the same size.
The tolerance values depend on module and diameter, so the same grade allows a few microns on a small pinion and considerably more on a large gear.
What a grade controls
- Pitchtooth-to-tooth and cumulative spacing
- Profileshape of the involute flank
- Helix (lead)alignment along the face width
- Runoutteeth concentric to the bore
- Not includedtooth thickness and backlash
How Do DIN, ISO and AGMA Grades Compare?
The systems measure similar deviations but number them differently. Use the table as orientation and always name the standard and its edition on the drawing.
| Standard | Grade range | Finer gear is | Notes |
|---|---|---|---|
| DIN 3961 / DIN 3962 | 1 to 12 | lower number | Common on German and European drawings |
| ISO 1328-1 | 1 to 11 (2013 edition), 0 to 12 (1995 edition) | lower number | Grade numbers broadly in line with DIN |
| AGMA 2000-A88 | Q3 to Q15 | higher number | Older US system; rule of thumb Q ≈ 17 minus the ISO grade |
| ANSI/AGMA ISO 1328-1 | A2 to A11 | lower number | Current US system, aligned with ISO |
Where a drawing lists profile, helix and pitch tolerances in microns, those values overrule a general grade.
Which Accuracy Grade Does Your Gear Need?
These are typical values, not rules. The right grade follows from speed, load, noise limits and the life you expect.
| Typical application | Usual grade (DIN / ISO) | Usual finishing |
|---|---|---|
| Slow open gears, conveyors, agricultural drives | 9 to 10 | Hobbed or shaped, often induction hardened |
| General industrial gearboxes and machine drives | 7 to 8 | Hobbed or shaped, through hardened or nitrided |
| Hardened industrial gearboxes, quiet or high-load stages | 5 to 6 | Case hardened and ground |
| High-speed gears, machine tools, master gears | 4 to 5 | Precision ground |
How Should You Specify Gear Accuracy?
- Name the standardWrite DIN 3962 or ISO 1328-1 with the grade, for example ISO 1328-1 grade 6.
- Give tooth thickness separatelyAdd the span or over-pin dimension with its tolerance. The grade does not cover backlash.
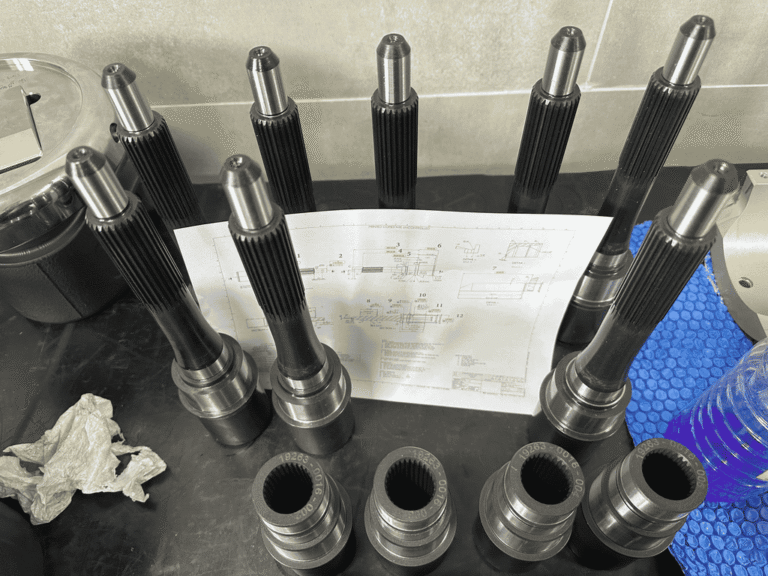
- State the referenceSay which bore or journals the teeth are measured from, and tolerance them to match.
- Match the pairGive both gears of a pair the same or a neighbouring grade.
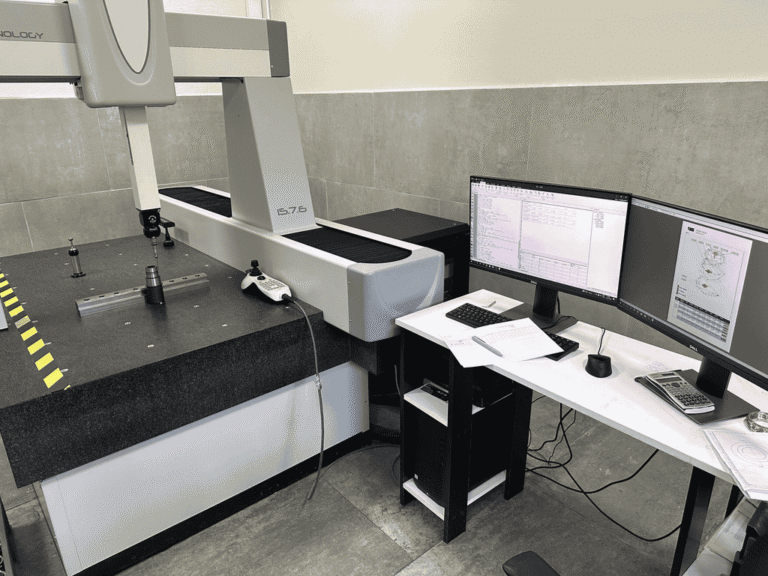
- Ask for the reportRequest profile, helix and pitch charts with the delivery if you need measured proof.
Why Does a Finer Grade Cost More?
Heat treatment distorts a gear. A case-hardened gear that left the hobbing machine at grade 8 comes out of the furnace coarser than it went in. Reaching grade 5 or 6 on a hardened gear therefore means grinding the flanks afterwards and measuring the result.
Hobbed and shaped gears
Good hobbing or shaping reaches around grade 8 to 9 on soft or pre-hardened steel. That is enough for a large share of industrial drives, and it avoids a grinding operation.
Ground gears
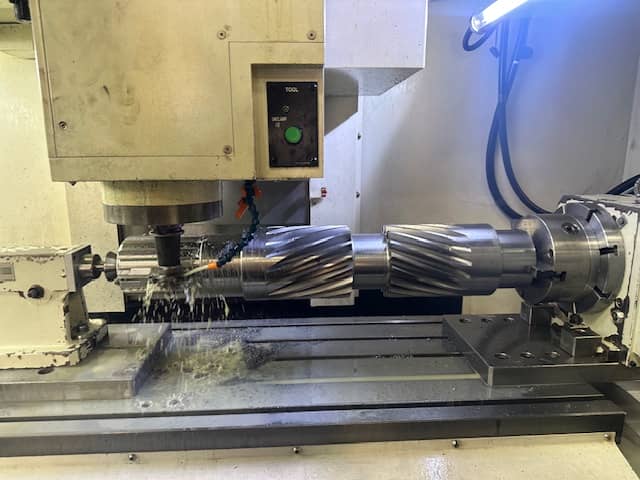
Grinding after hardening brings the teeth to grade 5 or 6 and allows profile and lead corrections such as tip relief and crowning. It adds machine time and inspection, which is why the grade should match the duty.
A practical rule
Do not copy the finest grade from an old drawing without asking why it was there. If the gear runs slowly under heavy load, material and heat treatment matter more than two grades of accuracy. If it runs fast or has to be quiet, the grade is worth paying for. Our quality page lists the reports we supply, and the machine park shows our grinding capacity.
Questions About Gear Quality Grades
Is DIN 3962 the same as ISO 1328?
No, but they are close. Both grade pitch, profile, helix and runout deviations, and both use lower numbers for finer gears. The tolerance values differ in detail, so the drawing should name one standard.
Which grade can gear hobbing reach?
Around grade 8 to 9 for hobbed or shaped gears, depending on size, module and material. Finer grades on hardened gears are reached by grinding.
Which grade can gear grinding reach?
Ground gears typically reach grade 5 to 6. We confirm the achievable grade for your part when we quote.
What is AGMA Q10 in ISO terms?
Roughly ISO grade 7. The rule of thumb for the older AGMA 2000 system is Q-number ≈ 17 minus the ISO grade. It is an approximation, not an exact conversion.
Does the accuracy grade include backlash?
No. Backlash comes from tooth thickness and centre distance tolerances, which are specified separately, in the DIN system to DIN 3967.
Need measured proof with the gears?
Gear measurement charts, hardness results and 3.1 material certificates are agreed at quotation.
Send a gear drawing. Get an answer within 24 hours.
Include the accuracy grade and standard, material, heat treatment and quantity. We reply with questions or a quotation.